

What a PCB hole inspection machine must answer
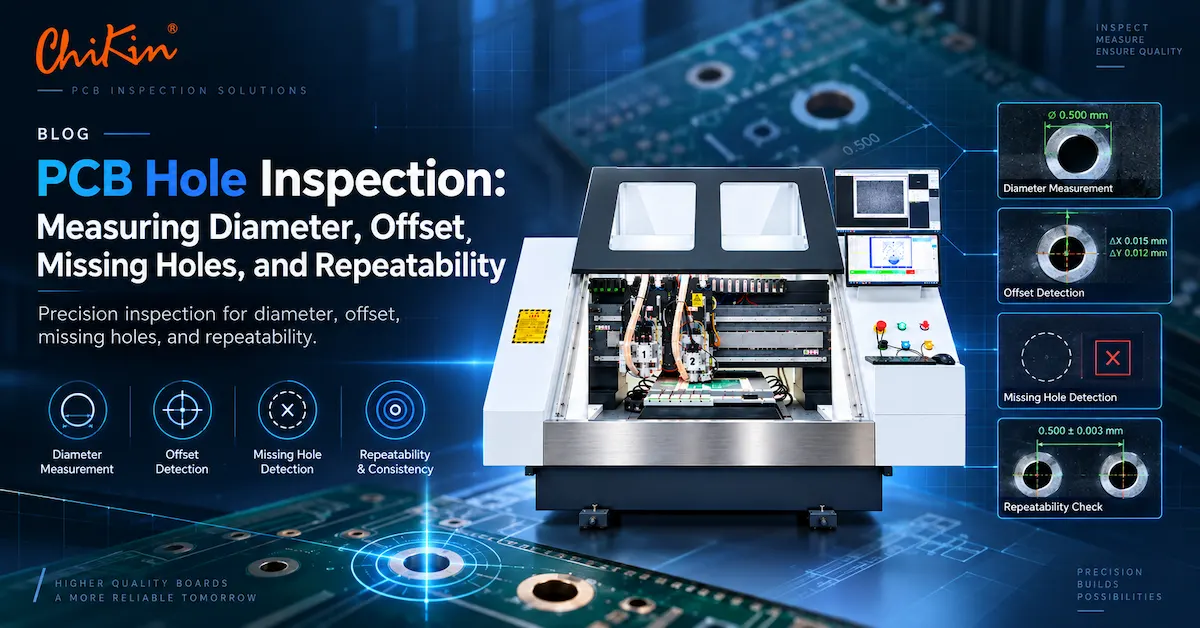
Hole inspection is often discussed as if it were one measurement. In a real factory, it is a group of decisions. The system must answer whether a hole exists, whether it is in the correct position, whether its diameter is within the required window, and whether the result remains stable when the board, tool, operator, or fixture changes. These questions have different causes and may need different optics, lighting, probing, software, or process controls.
| Inspection question | Typical defect | Evidence the buyer should request |
|---|---|---|
| Does the hole exist? | Missing hole, blocked hole, wrong drill program | Known-good and known-bad sample images, detection rate, false-call review |
| Is the hole in the correct position? | Offset, registration drift, tool deflection | Coordinate report referenced to fiducials or tooling holes |
| Is the diameter acceptable? | Oversize, undersize, taper, burr, resin smear | Measurement method, calibrated reference, min/max and repeatability data |
| Is the result repeatable? | Operator variation, fixture movement, lighting drift | Repeated measurements, range, standard deviation, gauge study |
These outcomes should be separated in the RFQ. For example, “inspection accuracy 0.01 mm” is incomplete unless the supplier explains whether it means camera pixel resolution, displayed resolution, repeatability, measurement uncertainty, or actual agreement with a calibrated reference. A high-resolution image can still produce an unreliable decision if the board is not flat, the edge is damaged, the lighting changes, or the software uses an unstable threshold.
Who needs this inspection capability
The immediate user may be a quality engineer, but the buying decision usually involves several people. The production manager wants throughput and simple operation. The process engineer wants stable registration and useful defect data. The quality team wants traceability and clear acceptance rules. The purchasing team wants a comparable quotation, delivery commitment, spare-parts plan, and supplier response. The end customer may want evidence that the hole pattern, diameter, and defect escape risk are controlled.
For that reason, a good inspection article and a good machine quotation should describe the manufacturer, product, material, application, and market clearly. CHIKIN CNC is a Shenzhen-based manufacturer of PCB drilling, routing, laser processing, and testing-related equipment. Its public product information includes CCD positioning, granite-base platforms, automatic tool handling, precision linear rails, and target drilling configurations. One public target-drilling page references a 0.15-3.175 mm drilling range, an approximately 560 x 680 mm table, and a plus or minus 0.005 mm repeatability claim. These are public reference points, not a substitute for a project-specific specification. The exact model, board stack, fixture, tool, and acceptance method should be confirmed in the quotation.
For buyers outside China, the “where” also matters. Ask where the machine will be built, where factory acceptance testing will occur, how remote support is delivered, where spare parts are stocked, and what installation or training is included. Those details often affect the real cost more than a small difference in headline machine price.
What materials and hole types change the inspection method
A measurement method that works on one board can fail on another. FR-4 can show resin smear, glass-fiber breakout, burrs, and changes in edge contrast. Aluminum-backed boards can create glare and a different contrast boundary. Flexible or rigid-flex materials can move under vacuum or clamping. Heavy copper, multilayer stacks, plated-through holes, microvias, slots, and counterbores all create different visual and dimensional conditions. The RFQ should therefore describe the material and finished condition, not only the nominal hole diameter.
Start by separating the hole population into families. A family may be defined by finished diameter, drill tool, plated or non-plated condition, board layer structure, or customer tolerance. A 0.20 mm microvia and a 3.175 mm tooling hole should not be treated as one measurement class. A plated-through hole may have a different finished diameter from the mechanical drill because copper plating changes the wall. A non-plated hole may need a different edge threshold because there is no copper barrel to define the boundary. Slots and routed openings may need a contour or width check rather than a circular diameter calculation.
| Board or feature | Main inspection risk | Useful control |
|---|---|---|
| FR-4 through hole | Resin smear, glass breakout, burr, wall damage | Stable coaxial lighting, sample images, edge-quality review |
| Plated-through hole | Finished diameter differs from drill size | Measure at the agreed process stage and define plating condition |
| Aluminum PCB | Reflective surface and thermal material contrast | Polarized or controlled lighting and a board-specific recipe |
| Rigid-flex or thin board | Movement, bow, local lift, registration shift | Fixture control, flatness check, fiducial registration |
| HDI or small hole group | Pixel limit, smear, crowded features | Optical validation with representative smallest features |
| Slot or routed opening | Width, length, corner and contour variation | Contour measurement and routing-process correlation |
Material information also helps the supplier choose the right machine architecture. A camera-based system may be ideal for presence and position, while a contact or optical metrology method may be needed for a tighter diameter requirement. A drilling machine with CCD positioning may prevent an offset before it becomes a downstream inspection failure. A separate inspection station may be better when several process steps must be audited or when the same line checks multiple product families.
How PCB hole diameter measurement should be specified
Diameter sounds straightforward: measure the circle and compare it with the drawing. The difficult part is defining which circle the system is measuring. The visible opening, copper edge, tool path, plated wall, and internal wall may not represent the same dimension. Before choosing a pcb hole diameter measurement solution, agree on the measurement location, board condition, reference artifact, and tolerance band.
A useful specification includes nominal diameter, lower limit, upper limit, measurement stage, board temperature, fixture condition, calibration frequency, and report format. If the requirement is 1.00 mm plus or minus 0.05 mm, write the complete rule as 0.95 to 1.05 mm at the finished inspection stage. If the dimension is a plated hole, state whether the measurement is before plating, after plating, or after any cleaning and surface treatment. If the customer drawing uses a hole class or a statistical process rule, include that rule rather than translating it into a generic “high accuracy” claim.
There are three common measurement approaches. The first is image-based measurement. It is fast, non-contact, and suitable for presence, position, and many diameter checks when the edge is visible and the board is stable. The second is contact measurement. It can be useful for selected reference parts or gauge studies, but it may be slower and may not represent every hole in a production panel. The third is process correlation. Here, the factory compares the machine result with a calibrated microscope, optical comparator, CMM, pin gauge, or customer-approved reference. The correlation step is critical because a repeatable wrong measurement is still wrong.
For an image-based system, the buyer should ask four questions. What is the smallest feature the camera can resolve under the actual material and lighting? How does the software define the edge when the wall has burrs or smear? How is board movement removed from the result? How are borderline images reviewed? A supplier that cannot explain these points may still have a useful machine, but the quotation is not yet technically complete.
Diameter data that belongs in the acceptance report
| Field | Why it matters | Example format |
|---|---|---|
| Hole ID | Links the result to the drawing or drill file | H-001, H-002, H-003 |
| Nominal | Defines the target dimension | 1.000 mm |
| Measured | Shows the actual result | 0.987 mm |
| Limit | Creates an objective pass/fail rule | 0.950-1.050 mm |
| Method | Prevents disputes about what was measured | Vision, pin, microscope, CMM |
| Recipe and date | Supports traceability | Recipe R03, 2026-09-28 |
| Image or evidence | Allows review of borderline features | Stored image or report link |
For high-volume production, do not only report the average diameter. The buyer should be able to see the minimum, maximum, range, and trend by tool, panel, stack, and time. A sudden shift in one tool family can indicate wear, runout, collet contamination, material movement, or a program problem. This is why diameter measurement becomes more valuable when it is connected with a maintenance and process-control workflow.
How to inspect hole position and offset
Hole position is usually a coordinate problem, not a simple image problem. A board can show a perfect circular opening and still fail because the opening is shifted relative to a pad, copper feature, slot, tooling hole, or customer datum. A useful pcb hole position inspection workflow must define the coordinate system first. The system should identify the drawing datum, fiducials, tooling holes, panel rails, or other registration references, then calculate the hole center in that same system.
Separate three sources of offset before changing the machine. Machine motion error can come from axis calibration, backlash, interpolation, spindle runout, or an incorrect work coordinate. Board registration error can come from panel movement, tooling-hole wear, vacuum weakness, fixture contamination, or a distorted panel. Material and process error can come from stack movement, thermal expansion, copper distribution, laminate movement, or a drilling tool that deflects under load. If these causes are mixed together, the corrective action may reduce one symptom while increasing another.
| Observed pattern | Likely cause to investigate | First verification |
|---|---|---|
| All holes shift in the same direction | Work zero, datum or fixture registration | Check fiducial and tooling-hole coordinate report |
| Offset changes across the board | Axis geometry, board movement or thermal effect | Compare center, corner and edge locations |
| One tool family shifts | Tool loading, collet, runout or program mapping | Repeat a small sample with a known tool |
| Only thin boards vary | Board lift, bow, clamping or vacuum issue | Measure flatness and fixture contact |
| Only plated features fail | Process-stage or layer-registration effect | Define pre-plating and post-plating references |
CCD positioning is valuable when the board contains reliable visual references. The camera does not eliminate the need for a good fixture or a stable board; it gives the control system a way to correct registration using visible references. During an RFQ, ask whether the camera finds fiducials automatically, how many reference points are recommended, how the system handles a missing or damaged fiducial, and whether the operator can review the correction before a production run.
A practical offset study uses at least three zones: center, corner, and the longest travel direction. Measure a defined number of holes in each zone, then calculate X error, Y error, radial error, and any directional pattern. If the results show a smooth increase toward one edge, look at geometry or board movement. If the results are random, look at repeatability, tooling, fixture stability, and measurement noise. If the results are consistent but biased, look at datum definition and compensation.
Why position accuracy and repeatability are different
Accuracy describes how close the result is to the reference value. Repeatability describes how close repeated measurements are to each other under the same conditions. A system can be repeatable but inaccurate if it uses the wrong datum or has a systematic offset. It can be accurate on average but poorly repeatable if the board moves or the image threshold changes. A serious purchase specification needs both terms.
Write the requirement in a way that can be tested. For example: “Using the supplied FR-4 sample, the approved fixture, the defined fiducial recipe, and the agreed measurement method, the machine shall measure the center of each selected hole within the specified X/Y tolerance, with repeated measurement range below the agreed value.” Avoid accepting a statement that only says “high precision CCD.” Ask for the sample size, coordinate reference, environmental condition, operator steps, and report output.
Missing hole detection is a presence decision
Missing hole detection should be tested with real defect samples. A system can detect a completely absent hole easily when the surrounding surface is clean, but the challenge is often a partially drilled hole, blocked hole, wrong layer condition, smear, burr, copper residue, or a hole placed in the wrong location. The buyer should therefore define the defect library rather than relying on one demonstration image.
The inspection recipe should know the expected hole map. That may come from a drill file, CAD data, Gerber data, a customer reference image, or a programmed coordinate list. The expected map tells the system where a hole should be. The image or sensor then confirms whether the feature exists and meets the required size or shape. This combination is stronger than simply searching for dark circles because it can detect an extra hole, a hole at the wrong coordinate, or a hole with an unexpected diameter.
| Defect sample | Why it matters | How to validate |
|---|---|---|
| Completely missing hole | Confirms basic presence detection | Use a controlled blocked or unprocessed sample |
| Partial hole or wrong depth | Tests threshold and edge logic | Use a sample with known visual difference |
| Wrong coordinate | Separates presence from position | Move a hole within the defined tolerance window |
| Oversize or undersize hole | Connects presence with diameter inspection | Compare with calibrated reference dimensions |
| Extra hole | Tests expected-map comparison | Insert an unprogrammed feature in a test sample |
False rejects matter as much as missed defects. If the system rejects good boards because of glare, dust, surface texture, or minor contrast variation, operators may begin overriding alarms. That creates a larger quality risk than a visible false call. Request a review screen, alarm image, defect coordinates, recipe version, and the ability to classify a false call. The supplier should explain how lighting, focus, exposure, board flatness, and cleaning are controlled.
PCB drill inspection must connect to the process
A downstream pcb drill inspection station is most useful when it gives the drilling process feedback. The purpose is not only to sort good and bad boards. The data should help the factory identify tool wear, broken drills, incorrect tool loading, spindle runout, collet contamination, vacuum problems, fixture movement, and program mistakes before the defect becomes a customer escape.
For example, if hole diameter gradually increases for one tool family, the maintenance response may be different from a sudden shift affecting every hole. If only one corner of the panel shows offset, the response may focus on fixture contact or board movement. If the missing-hole pattern matches one tool number, the response may focus on tool break detection and tool-change confirmation. A useful report makes these patterns visible instead of reducing everything to a green or red screen.
Ask whether the inspection system can export CSV, PDF, image evidence, or a machine-readable result. Ask whether the report includes board ID, panel ID, recipe version, operator, time, defect coordinate, measured value, limit, and disposition. If the factory uses MES or a quality database, confirm the communication method before purchasing. A system that stores only a local image may be acceptable for a small workshop but insufficient for a traceable high-volume line.
How to prove repeatability before you buy
Repeatability is one of the most important and most misunderstood parts of a machine quotation. A displayed resolution does not prove that the system can produce the same result repeatedly. To evaluate repeatability, repeat the same measurement or inspection under controlled conditions and quantify the spread. Then repeat the exercise after a board change, operator change, fixture reload, or recipe reload if those events are part of normal production.
A practical study can start with ten to thirty selected holes across a representative board or panel. Choose small, medium, and large diameters; center and edge locations; different tool families; and any high-risk features. Measure each feature several times without changing the board, then reload the board and repeat. If the machine is intended for multiple shifts, include an operator handoff or a controlled time interval. The purpose is not to create a laboratory experiment. It is to measure the conditions that will actually affect purchasing risk.
| Study step | What to record | Decision value |
|---|---|---|
| Reference setup | Board, fixture, recipe, tool, temperature | Defines the test condition |
| Repeated measurement | Each result for each selected hole | Shows short-term repeatability |
| Board reload | New registration result after reload | Shows fixture and datum sensitivity |
| Operator change | Result by trained operator | Shows workflow robustness |
| Reference comparison | Approved gauge or microscope result | Shows agreement and bias |
| Pass/fail decision | Range, average, bias, false calls | Connects data to acceptance |
For diameter measurement, look at range, average, bias against the reference, and the percentage of decisions that change when the same feature is measured again. For position, look at X, Y, and radial error separately. For missing-hole detection, look at true positives, false negatives, and false positives. A supplier may use different statistical terminology, but the buyer should still receive plain-language results and the raw sample conditions.
Repeatability questions for an RFQ
- What is the smallest hole or feature included in the repeatability claim?
- Is the claim a resolution, accuracy, repeatability, or measurement uncertainty value?
- What board material, thickness, surface finish, and condition were used?
- Was the board reloaded between measurements?
- How many holes and boards were included?
- Was the result compared with a calibrated reference?
- How are borderline values and false calls reviewed?
- What calibration or cleaning routine is required?
If the supplier has no ready-made study, include it in the factory acceptance test. The acceptance plan should name the sample board, the defect samples, the measurement points, the pass/fail limits, the report format, and what happens if the machine does not meet the agreed result. This protects both buyer and supplier because the same method is used to judge performance.
Choosing between a drilling machine, an inspection station, and both
Some buyers need inspection only. Others need a drilling platform with CCD positioning, tool monitoring, and process controls that reduce defects before inspection. The right choice depends on where the quality problem starts.
| Situation | Likely first investment | Why |
|---|---|---|
| Existing boards show missing or extra holes | Inspection and expected-map verification | Finds escapes and separates program errors from machine errors |
| Hole centers drift after setup or board reload | CCD registration and fixture improvement | Controls the datum before drilling or inspection |
| Diameter changes with tool life | Drilling process monitoring plus measurement | Connects tool condition with finished size |
| Throughput is limited by one spindle | Multi-spindle drilling or routing | Increases parallel processing after quality is stable |
| Several customers require traceability | Inspection reporting and data integration | Provides evidence by board, recipe and time |
CHIKIN's public product catalog includes single-spindle, one-drilling-one-routing with CCD, two-spindle, four-spindle, target drilling with CCD, and testing/inspection equipment categories. The public catalog also references automatic tool change, tool-length or broken-tool detection, granite bases, and precision positioning on selected configurations. A buyer should compare these features by application rather than selecting a spindle count or camera specification in isolation.
For a mixed job shop, a single-spindle or combined drilling/routing machine may be more flexible. For a stable, high-volume board family, two or four spindles may make more sense if the board size, tool library, fixture, and cycle time support the investment. For target-hole registration, a CCD-equipped target drilling platform may be more relevant than a generic inspection camera. For final defect sorting across many process steps, a dedicated testing or inspection station may be the better fit.
What to include in a high-quality PCB hole inspection RFQ
A vague RFQ produces vague quotations. The supplier needs enough information to recommend the correct sensor, fixture, software, and machine configuration. The buyer also needs enough information to compare different suppliers on the same basis.
| RFQ section | Information to provide |
|---|---|
| Product | PCB type, application, board family, panelization, customer market |
| Material | FR-4, aluminum, rigid-flex, copper, thickness, surface condition |
| Features | Hole diameter range, slots, tooling holes, fiducials, plated/non-plated condition |
| Tolerance | Diameter limits, X/Y offset, missing-hole rule, repeatability target |
| Throughput | Boards per hour, holes per board, shift pattern, changeover frequency |
| Evidence | Sample boards, known-good images, known-bad samples, reference measurements |
| Integration | CSV/PDF/MES output, barcode, recipe control, operator permissions |
| Factory | Power, air, vacuum, floor area, temperature, network, dust control |
| Commercial | Lead time, packaging, installation, training, spare parts, warranty, service |
Include at least one real sample or a detailed drawing. If the supplier cannot test the actual board, ask for the limitation to be written into the quotation. A machine may meet a headline optical specification and still be unsuitable for a particular copper finish, board warp, hole wall condition, or throughput target.
Factory evidence that makes the article useful to buyers
Technical advice becomes more credible when the buyer can see how the manufacturer connects the machine to a real production workflow. Product images are useful, but a product image alone is not evidence of measurement performance. Strong evidence includes a clear machine view, a factory or packaging scene, a sample report, a test board, a calibration or reference method, and an explanation of what the engineer checks before shipment.
In a project discussion, ask the manufacturer to show the following items when available: the machine configuration that matches the quotation, the workholding area, the camera or sensor location, the lighting arrangement, the operator screen, a representative board, the defect image library, the report output, and the packaging method. If the equipment will be exported, ask for the planned crate or packaging standard, moisture protection, shock protection, spare-parts packing, and installation instructions. CHIKIN's media library includes product, factory, packaging, and after-sales service images that can help buyers understand the supplier's equipment and support workflow. The final project evidence should still be tied to the selected model and customer sample.
Do not turn a factory photograph into an unsupported case study. A responsible article can say what the picture shows and what the buyer should ask next. For example, a packaging image may show that the supplier prepares equipment for shipment, but it does not prove a particular delivery time or damage-free arrival. A service image may show the support workflow, but it does not replace a written warranty and response agreement. A product image may show a CCD-equipped drilling platform, but it does not prove the exact accuracy for every PCB material.
Recommended evidence block for a supplier page
| Evidence | Buyer question | How to keep it honest |
|---|---|---|
| Product photograph | What machine configuration is shown? | Identify model or state that configuration may vary |
| Factory scene | Where is the equipment assembled or prepared? | Use a current image and give a date or context |
| Sample report | What fields and decisions are recorded? | Remove customer confidential data and show units |
| Test board | Was the buyer's material tested? | Show material, thickness, feature range and result |
| Packaging image | How is the machine protected for export? | Describe packaging scope without promising carrier performance |
| Engineer note | What commonly causes false calls or drift? | Use practical observations and mark configuration limits |
This approach also helps search engines and AI systems understand the entity behind the page. The page should make it clear that CHIKIN CNC is the manufacturer or equipment supplier, what it produces, where it operates, which PCB materials and applications it supports, and how a buyer can request a configuration review. Clear entity information is not decorative. It reduces ambiguity when a buyer searches for a machine, a factory, a product family, or a supplier comparison.
How to compare suppliers without being misled by headline accuracy
Supplier comparison is a commercial investigation, not a contest for the smallest number in a specification table. Compare the complete measurement chain: board registration, fixturing, sensor, lighting, software, calibration, reporting, operator steps, maintenance, and service. Ask every supplier to use the same test board and acceptance method. If one supplier reports camera resolution and another reports repeatability, the numbers cannot be compared directly.
Check whether the supplier explains what happens when the system sees a borderline hole. Can the operator zoom into the feature? Can the system store the image? Can the operator remeasure without changing the original result? Can a quality manager approve a disposition? Can the recipe be protected from unauthorized changes? These workflow details determine whether the machine remains useful after the initial installation.
Also compare the total cost of ownership. A lower purchase price may become expensive if the factory needs frequent manual cleaning, expensive light sources, special fixtures for each board, paid software options, difficult calibration, or slow remote support. A higher initial price may be reasonable if it includes a stable fixture, sample validation, operator training, spare parts, report integration, and a clear acceptance process. Request a written list of included and optional items.
Common failure modes and practical fixes
| Failure mode | What it looks like | Practical response |
|---|---|---|
| Glare or unstable contrast | Good holes alternate between pass and fail | Control lighting, surface angle, exposure and board cleaning |
| Board movement | Position errors change after reload | Improve fixture contact, vacuum, pins and datum registration |
| Tool wear | Diameter or wall quality drifts with production count | Track tool life, inspect runout and correlate with measurement data |
| Resin smear or burr | Edge threshold becomes ambiguous | Define edge rule, clean sample, and validate with approved reference |
| Wrong recipe | Unexpected holes or dimensions are not detected | Use recipe control, barcode or operator confirmation |
| False missing-hole call | Dust, shadow or reflection creates an alarm | Review defect images and set a cleaning and lighting routine |
| No traceability | Result cannot be linked to board or operator | Add board ID, recipe, timestamp and report storage |
Most of these problems are not solved by increasing camera megapixels alone. They are solved by matching the inspection method to the material and production process, controlling the reference, and making the result visible to the people who must act on it.
Applications by market and production stage
The same inspection language can mean different things in different markets. A prototype shop may need fast verification after a program change and may accept more manual review. An automotive supplier may need stronger traceability, controlled recipes, and evidence for customer audits. An LED or aluminum-board producer may need lighting and material validation that differs from a standard FR-4 workflow. A high-density interconnect supplier may prioritize small-feature resolution and registration. A contract manufacturer may need to support many board families with quick changeover.
| Market or application | Quality priority | Questions for the supplier |
|---|---|---|
| Prototype and NPI | Fast setup and engineering visibility | How quickly can a new board recipe be created and verified? |
| Consumer electronics | Throughput and false-call control | What is the cycle time at the required hole count? |
| Automotive electronics | Traceability and process evidence | What reports, permissions and audit records are available? |
| LED and aluminum PCB | Reflection, flatness and material variation | Can the supplier test the actual aluminum or metal-backed board? |
| HDI and fine features | Small-feature measurement and registration | What is the validated smallest feature, not only the camera pixel size? |
| Job-shop production | Changeover and recipe flexibility | How are multiple materials and board sizes handled? |
When the application changes, the machine recommendation may change as well. A system that is technically capable of measuring a small hole may not be commercially sensible if the line needs hundreds of board changes per day. A high-throughput machine may not be appropriate if the critical risk is a small, customer-specific registration feature. The best buying decision balances measurement risk, throughput, changeover time, labor, service, and future product mix.
Delivery, installation, training, and after-sales questions
Inspection equipment is a production system, not only a boxed device. Before issuing a purchase order, ask for the expected manufacturing and delivery schedule, what information the buyer must provide, how factory acceptance testing is organized, and which activities are included after arrival. The supplier should explain installation requirements, power, air or vacuum, network, temperature, floor space, operator training, maintenance, calibration, and spare parts.
For an export project, packaging should be included in the technical and commercial discussion. Confirm the crate dimensions, gross weight, moisture protection, shock protection, lifting points, documentation, and whether spare parts are packed separately. Ask who is responsible for customs documents and whether the supplier provides a packing list, electrical diagram, software backup, and maintenance schedule. A clear shipment package reduces delays when the machine reaches the factory.
After-sales support should also be measurable. “Global support” is a useful starting statement, but the RFQ should define contact channels, working hours, remote diagnosis method, response target, escalation path, spare-parts availability, and what is excluded from warranty. CHIKIN's public materials describe remote support, installation guidance, training, spare-parts support, and after-sales service. Its website also contains different warranty and precision statements on different pages, so buyers should ask for the exact warranty language for the selected model and configuration.
A buyer-ready acceptance plan
The acceptance plan should be written before the machine is shipped. It can be short, but it must be specific. A useful plan includes the board drawing, sample quantity, hole population, defect samples, fixtures, recipes, measurement reference, environmental conditions, cycle-time target, report fields, and pass/fail rules.
- Approve the sample board and confirm material, thickness, surface condition, and hole population.
- Approve the fixture, datum, fiducial or tooling-hole reference.
- Define the diameter, position, missing-hole, extra-hole, and repeatability limits.
- Run a known-good sample and record the full report.
- Run controlled defect samples and record true calls and false calls.
- Repeat selected measurements after reload and operator handoff.
- Review cycle time, changeover time, cleaning steps, and operator actions.
- Confirm the report export, image storage, recipe backup, and user permissions.
- Document any open items, responsible party, and completion date.
This plan protects both sides. The buyer receives evidence that matches the intended production use. The supplier receives a clear target instead of a general request for “high accuracy.” If the board or process changes later, the same plan can be revised and used for a new validation.
What to ask for in your quotation
Ask the supplier to separate machine hardware, software, fixtures, options, training, shipping, installation, spare parts, and recurring costs. Request the model number, configuration drawing, working area, supported board thickness, hole range, sensor or camera information, lighting, registration method, report format, cycle time assumptions, power, air or vacuum requirements, and maintenance schedule. Ask which figures are guaranteed, which are typical, and which depend on sample validation.
For a targeted quotation from CHIKIN CNC, send the board material, maximum board size, thickness, smallest and largest hole, plated or non-plated condition, expected holes per board, daily volume, required tolerance, available sample files, and the destination country. Add photographs or drawings of difficult features. This allows the engineering team to recommend whether a target drilling machine with CCD, a drilling/routing platform, a dedicated testing/inspection machine, or a combined workflow is more appropriate.
The strongest enquiry is not “How much is a PCB hole inspection machine?” It is: “We need to verify these hole families on this material, at this volume, with these limits. Please recommend the configuration, test our sample, provide the measurement method and repeatability report, and quote the complete delivery and support scope.” That question gives the supplier enough information to respond with a useful proposal instead of a generic price.
Buyer FAQ about PCB hole inspection
What is a pcb hole inspection machine?
It is a machine or inspection station that verifies PCB holes against a defined map, dimension, coordinate reference, and acceptance rule. Depending on the configuration, it may use cameras, controlled lighting, probes, gauges, or a combination of methods. The important point is the decision process, not the label alone.
Is a drilling machine the same as a hole inspection machine?
No. A drilling machine creates holes. An inspection machine checks whether the result matches the expected condition. Some drilling platforms include CCD positioning, tool monitoring, or process checks that reduce risk, but a separate inspection station may still be needed for final verification or traceability.
Can one system measure diameter and position?
Often yes, if the optics, fixture, software, and board condition support both measurements. The buyer should confirm the validated range and the measurement reference. Position can be calculated from fiducials or tooling holes, while diameter requires a stable and defined edge condition.
How does missing hole detection work?
The system compares an expected hole map with the observed board. It should identify absent, extra, misplaced, blocked, or visually ambiguous features according to the programmed rule. Known-good and known-bad samples are required to prove the rule.
What causes false missing-hole alarms?
Common causes include glare, dust, shadow, board movement, surface texture, poor focus, unstable exposure, resin smear, and an incorrect recipe. Cleaning and lighting control are as important as the camera specification.
How do I define pcb hole diameter measurement?
State the nominal size, lower and upper limits, process stage, material, plated or non-plated condition, reference method, calibration method, and report fields. Do not use “high precision” as the only requirement.
What does repeatability mean in a quotation?
Repeatability describes the spread of repeated results under the same defined conditions. Ask for the sample size, board, fixture, operator workflow, measurement method, and whether the board was reloaded. Confirm that repeatability is not being confused with display resolution.
Do I need CCD positioning?
CCD positioning is useful when board registration or target-hole alignment is a major risk and reliable fiducials or tooling references are available. It does not replace a stable fixture, clean reference, or correct board design data.
What board materials should be tested before purchase?
Test the actual materials and surface conditions that will run in production, such as FR-4, aluminum-backed PCB, rigid-flex, heavy copper, or plated and non-plated variants. A supplier demonstration on a different board may not predict your result.
How many sample holes should be in an acceptance test?
There is no universal number. Include the smallest, largest, most critical, center, edge, and long-travel features, plus the hole families that create the most customer risk. The supplier and buyer should agree on the sample before the test.
Should I buy AOI, BBT, a flying probe tester, or a hole inspection system?
Choose based on the failure you need to detect. AOI focuses on visual or pattern-related defects. BBT and flying probe systems focus on electrical continuity and isolation. Hole inspection focuses on hole presence, position, dimension, or related mechanical results. Some factories need more than one type.
How can I compare suppliers fairly?
Use the same sample board, feature list, limits, cycle-time target, reporting requirements, and acceptance method. Compare the complete system and support scope, not only a headline accuracy number or machine price.
What information should be sent with an RFQ?
Send board material, dimensions, thickness, hole range, plating condition, files or drawings, production volume, tolerance, sample images, destination country, power conditions, and desired delivery date. Include the specific defects that must be detected.
What should be included in the final quotation?
The model, configuration, fixtures, software, options, test method, guaranteed values, typical values, lead time, packaging, installation, training, spare parts, warranty, support process, and exclusions should be clear. Ask the supplier to mark any value that depends on sample validation.
Can CHIKIN CNC test my PCB sample?
Request a sample evaluation with your actual material, thickness, hole range, and defect examples. The public CHIKIN catalog includes PCB drilling, routing, target drilling with CCD, and testing or inspection equipment, but the correct configuration depends on the application and should be confirmed by engineering review.
Final checklist before sending a purchase enquiry
- We defined whether the intent is inspection, prevention, or both.
- We separated diameter, position, missing-hole, and repeatability requirements.
- We described the real board material, thickness, finish, and hole families.
- We prepared known-good and known-bad sample information.
- We defined the coordinate reference and measurement stage.
- We requested a repeatability and false-call study.
- We requested report fields, image evidence, and traceability.
- We compared fixture, lighting, software, maintenance, and service scope.
- We wrote an acceptance plan before shipment.
- We included delivery, packaging, training, warranty, and support questions.
In short: the best pcb hole inspection machine is not the one with the largest headline number. It is the system that measures the features your customers care about, uses the correct reference, produces stable decisions on your real materials, records evidence, and gives your team a practical way to act on drift.